

service hotline:
+86 18929311368
+86 18929311368
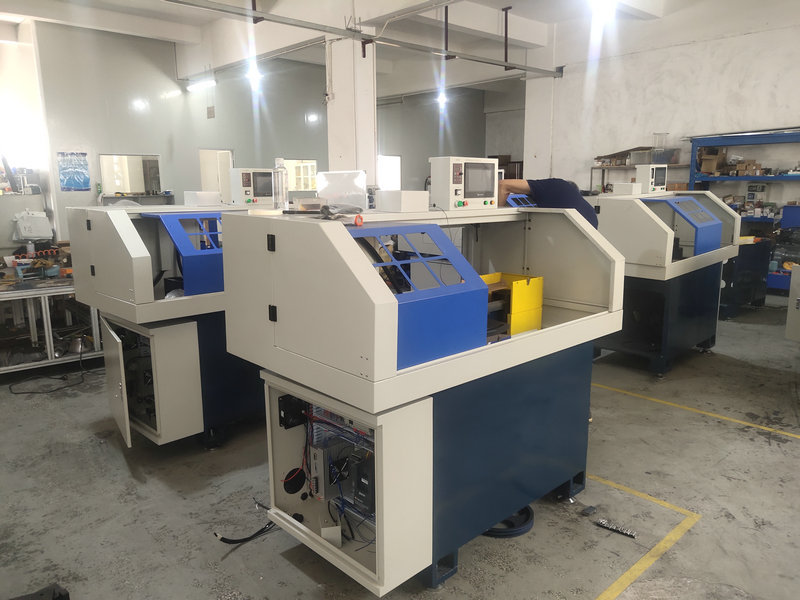
Gear processing process:
1. Forging and making blank
Hot die forging is still a widely used blank forging process for automotive gear parts. In recent years, wedge rolling technology has been widely used in shaft machining. This technology is especially suitable for the more complex step shaft production, it is not only high precision, small post-processing allowance, but also high production efficiency.
2. Normalize
The purpose of this process is to obtain a hardness suitable for the cutting of the rear sequence gear and prepare the structure for the final heat treatment to effectively reduce heat treatment deformation. The material used for gear steel is usually 20CrMnTi, the general normalizing due to the influence of personnel, equipment and the environment is relatively large, making the cooling speed and cooling uniformity of the workpiece difficult to control, resulting in large hardness dispersion, metallographic organization is not uniform, directly affecting the metal cutting processing and final heat treatment, making the thermal deformation is large and irregular, parts quality can not be controlled. For this reason, isothermal normalizing process is adopted. Practice has proved that the use of isothermal normalizing has effectively changed the disadvantages of normal, and the product quality is stable and reliable.
3. Turning processing
In order to meet the positioning requirements of high-precision gear machining, all the processing of the tooth blank adopts CNC lathe, the use of mechanical clamping and no heavy grinding tool, to achieve a simultaneous completion of the aperture, end face and outer diameter processing under one clamping, which not only ensures the perpendicularity requirements of the inner hole and the end face, but also ensures the size of the mass of the tooth blank production. Thus, the precision of the blank is improved and the machining quality of the rear sequence gear is ensured. In addition, the high efficiency of CNC lathe processing also greatly reduces the number of equipment, and the economy is good.
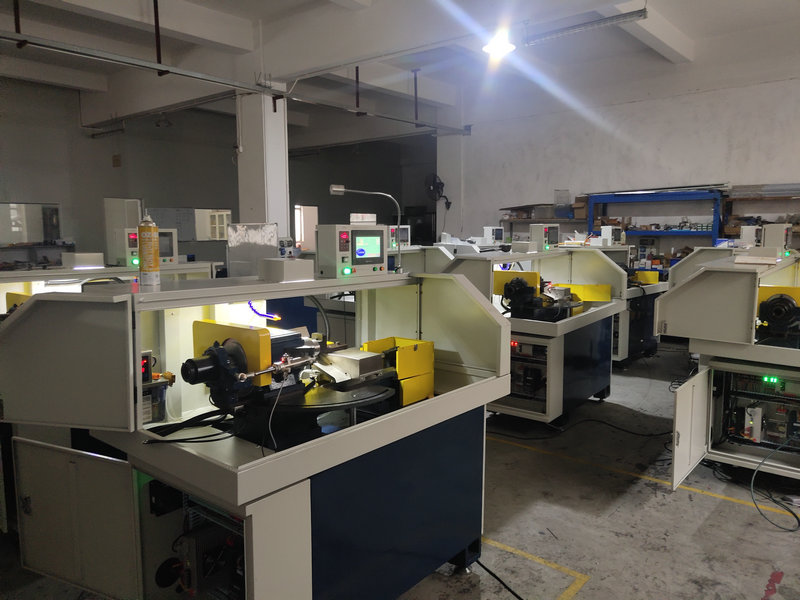
4. Roll and gear shaping
The equipment used for processing teeth is still a large number of ordinary gear hobbing machine and gear shaper machine, although the adjustment and maintenance is convenient, but the production efficiency is low, if the completion of large capacity requires multiple machines to produce at the same time. With the development of coating technology, the re-coating of hob and insert blade after grinding is very convenient, and the service life of the coated tool can be significantly improved, generally by more than 90%, effectively reducing the number of tool changes and sharpening time, and the benefits are significant.
5. Shave teeth
The radial shaving technology is widely used in the production of automobile gear for its advantages of high efficiency, easy realization of the shape and direction modification requirements. Since the company bought the special radial shaving machine from the Italian company in 1995, the technology has been applied in this technology, and the processing quality is stable and reliable.
Step 6 Heat treatment
Automobile gear requires carburizing and quenching to ensure its good mechanical properties. For products that are no longer grinding after heating, stable and reliable heat treatment equipment is essential. The company introduced the continuous carburizing and quenching production line of German Lauyi Company, and obtained satisfactory heat treatment results.
7. Grinding processing
It is mainly to finish the inner hole, end face and outer diameter of the shaft of the gear after heat treatment, so as to improve the dimensional accuracy and reduce the form and position tolerance.
Shenzhen Chuwang Automation Co., LTD
Landline: 0755-27193983
Phone: 18929311368 Mr. Yan
Website: www.szchuwang.com
Add: 1st Floor, Building B1, Youbang Industrial Park, Fourth Industrial Zone, Tianliao Community, Yutang Sub-district, Guangming District, Shenzhen City

 0755-27193983
 QQ
 Wechat

 con

